A REPEATABLE METHOD
How to use it
- Define the comparison and reference before touching the dial. Use an already loose part on a safe manual bench fixture, with marked measurement positions and a documented support arrangement. Do not mount the indicator on moving, energised or stored-energy equipment; machinery work needs a separately competent isolation and measurement process.
- Identify the exact plunger model, units, division value, range and revolution counter where present. Inspect the contact point and clean accessible contact/reference surfaces by the applicable instructions. A chip under the sample or a loose support can become part of the reading rather than a feature of the part.
- Use the manufacturer-approved mounting arrangement without distorting the stem, and align the spindle with the intended displacement direction. Keep a suitable initial contact position within the model’s working range; do not apply a universal preload or clamping torque. A lever indicator has different contact geometry: its angle correction is not interchangeable with this setup.
- At the reference position, note the initial reading or set the bezel reference according to the manual, then verify smooth return to that same reference. Move only the safely supported manual sample or fixture as intended, avoid lateral force on the spindle and stay within travel. Record positions and signed readings; do not force a sticky mechanism or push through the end stop.
- Return to the same reference and repeat the comparison with unchanged support, direction and contact conditions. Retain a zero-return shift or spread between repeats instead of hiding it with another zero adjustment. If the reference is unstable, stop and resolve the setup or obtain competent metrology help before using the figures for acceptance.
INTERPRET THE MEASUREMENT
How to read the result
- Fictional signed readings −0.02 mm and +0.18 mm have a spread of 0.18 − (−0.02) = 0.20 mm, not 0.16 mm. This is the spread of those observations. It is not automatically true geometric runout, flatness or an eccentricity of 0.10 mm.
- A fictional 0.01 mm division corresponds to 10 µm. Twenty such divisions correspond to 0.20 mm. Division value is not an accuracy of ±0.01 mm; consult the actual indication-error, repeatability and calibration information for the model and setup.
- Changing the zero reference shifts individual readings but does not change their spread: +0.48 mm and +0.68 mm still span 0.20 mm. A successful return to zero is a useful setup check, not an independent calibration or proof of compliance with a drawing.
- Record the measurement direction, signed values, units, sample support, positions, contact point and return check together. The dial alone cannot separate part variation from fixture movement, angular misalignment, contact deformation or dirt. Use only the capability demonstrated by the complete measurement method.
TROUBLESHOOT THE METHOD
Common problems and what to check
The pointer does not return to the reference.
Stop accepting results. Check the safely accessible support and contact conditions, and follow the model’s care guidance. Do not zero again to hide drift, add oil by guesswork or open the mechanism; seek the manufacturer’s service advice if motion remains poor.
The pointer makes more than one revolution.
Read the instrument’s full travel indication and revolution counter as its manual requires. Do not interpret the large pointer alone or treat a completed revolution as zero displacement.
Readings change after touching the stand or moving the part.
Document the changed condition and re-establish a stable comparison. An unstable fixture is not corrected by quoting more decimal places or borrowing a lever-indicator cosine correction.
STOP BEFORE THE HAZARD
Safety boundary
- This page covers loose-part manual bench observation only. Do not reach near a running spindle, fan, saw or vehicle drivetrain, and do not improvise a machine-isolation procedure from a measurement article.
- Use a stable support and handle sharp or heavy parts with an appropriate safe process. Do not rely on a magnetic base on an unsuitable surface or allow a fixture to fall onto the sample or your hands.
- Do not repair or modify the indicator or claim a structural, machine-alignment or precision acceptance decision from this illustrative exercise. A tighter tolerance requires an appropriate verified measurement method, not a finer-looking dial.
SMART BUYING GUIDE
What to look for when choosing
- Match working travel, units and documented measurement performance to the actual comparison, not the smallest printed division alone.
- Check suitable mounting, contact geometry and a rigid compatible support. A bare indicator without an adequate fixture is not a complete measuring setup.
- Check model-specific care, orientation limitations and calibration/service support. Do not transfer a clamp limit or a digital zero-setting rule from another model to a mechanical indicator.
Types of tool
Best for: A documented axial displacement comparison within its working travel, with the appropriate manual support.
Best for: A compatible method needing the documented display or data functions; extra digits do not eliminate alignment or fixture errors.
Common functions
Worth paying more for
- Documented performance, usable travel and service/calibration support.
- A compatible stable fixture and contact arrangement for the task.
Usually not worth the extra cost
- Extra display resolution without sufficient accuracy or support rigidity.
- Assumed equivalence between a lever test indicator and a plunger indicator.
Sources & instructions
- Mitutoyo Quick Guide, PG30: plunger mounting, alignment, motion and reference checks (English, single-page PDF; model-specific numbers are not universal)
- Mitutoyo Quick Guide, PG27: plunger parts, dial faces and revolution counting (English, single-page PDF)
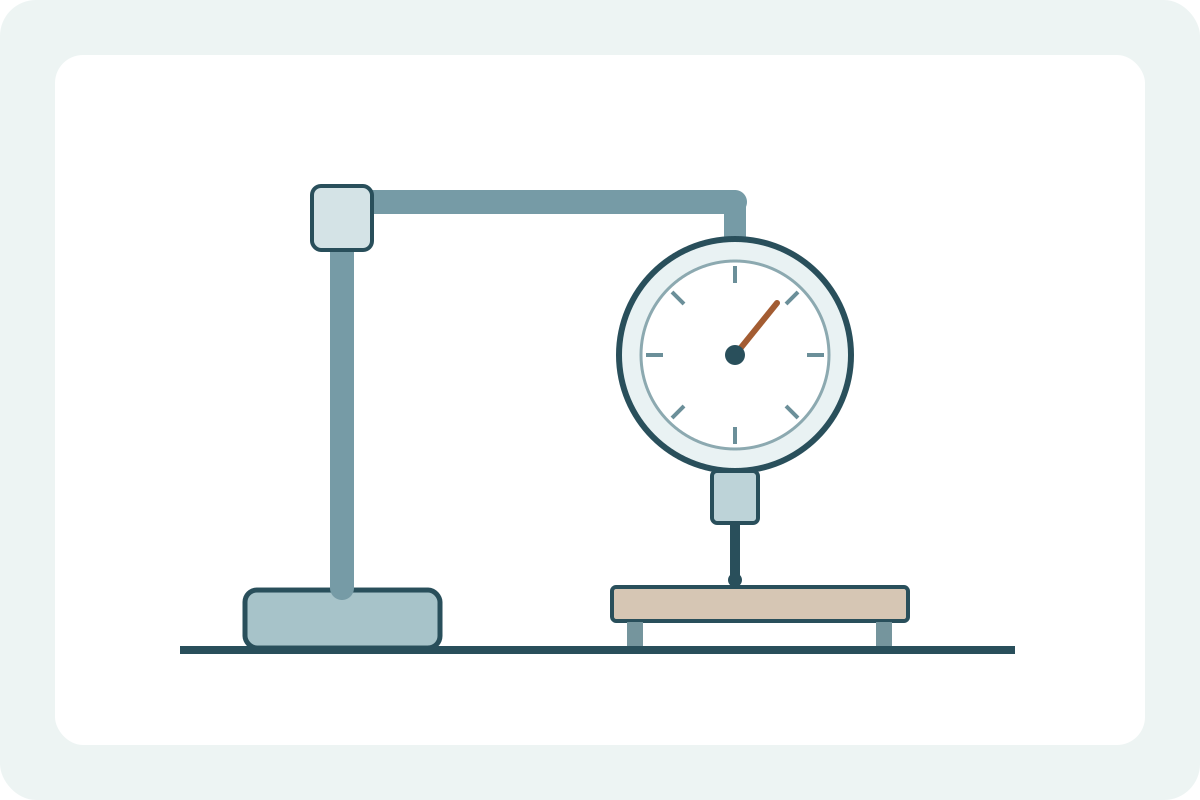
Original schematic, not a photograph, assembly instruction or calibration reference. The dial has no usable scale and gives no tolerance or fixture dimensions.